Liquid Ring Vacuum Pumps: Working Principle, Applications, and Maintenance
Liquid Ring Vacuum Pumps play an important role in many industrial processes where reliable vacuum generation is essential. These pumps are widely used across industries such as chemical processing, food production, wastewater treatment, pharmaceuticals, and manufacturing.
Choosing the right vacuum technology can improve operational efficiency, support consistent performance, and reduce unnecessary maintenance requirements.
In this guide, we explore how Liquid Ring Pumps work, their major applications, key benefits, and important maintenance considerations to help you make an informed decision.
What Are Liquid Ring Vacuum Pumps?
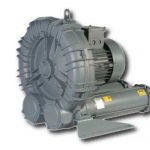
Liquid Ring Vacuum Pumps are positive displacement pumps that use a rotating liquid, usually water, to create a vacuum. They feature an impeller positioned eccentrically inside a cylindrical casing, allowing the operating liquid to form a rotating ring during operation.
PumpAir Solutions supplies Liquid Ring Vacuum Pumps from established manufacturers, including Pompetravaini and Gardner Denver Nash, for various industrial vacuum requirements across Australia.
How Do Liquid Ring Pumps Work?
Understanding the working principle of Liquid Ring Pumps helps explain why they are suitable for demanding industrial environments.
The operating process involves several steps:
- Liquid Supply: The pump casing receives a supply of operating liquid, commonly water, which acts as the sealing medium.
- Impeller Rotation: An eccentrically positioned impeller rotates inside the pump casing, creating centrifugal force that pushes the liquid towards the casing walls.
- Formation of the Liquid Ring: The rotating liquid forms a ring around the inside of the casing. The space between the impeller blades and liquid ring creates individual chambers.
- Gas Intake: As the chamber volume increases, gas enters through the suction port.
- Gas Compression: Continued impeller rotation reduces the chamber volume, compressing the trapped gas.
- Gas Discharge: The compressed gas is released through the discharge port, usually along with some operating liquid. The cycle then repeats.
This continuous process allows Liquid Ring Vacuum Pumps to generate and maintain vacuum conditions for a wide range of industrial applications.
Common Industrial Applications of Liquid Ring Vacuum Pumps
Liquid Ring Pumps are used in industries that require dependable vacuum performance, particularly where moisture or vapours are present. Some common applications include:
1. Chemical Processing
Chemical manufacturing processes often involve vapours, moisture, and demanding operating conditions. Liquid ring technology can provide suitable vacuum performance for applications such as distillation, solvent recovery and vacuum processing, subject to appropriate material selection.
2. Food and Beverage Processing
These pumps are used in various food production processes, including evaporation, filtration, vacuum packaging and processing operations where suitable hygienic system design is required.
3. Wastewater Treatment
Industrial wastewater treatment facilities may use vacuum equipment for filtration, dewatering and other process operations. Liquid Ring Vacuum Pumps can be considered where the process involves moisture and compatible gas streams.
4. Pharmaceutical Manufacturing
Vacuum technology supports processes such as drying, filtration, and solvent recovery in pharmaceutical manufacturing. Appropriate pump materials and operating conditions must be selected according to process requirements.
5. Paper and Manufacturing Industries
Liquid Ring Pumps are also used in paper manufacturing, plastic processing, industrial drying, and other production environments where consistent vacuum performance is required.
Single-Stage vs Two-Stage Liquid Ring Vacuum Pumps
Liquid Ring Vacuum Pumps are available in single-stage and two-stage configurations.
Single-Stage Liquid Ring Pumps: These pumps compress gas through one pumping stage. They are suitable for many general industrial vacuum applications where the required operating vacuum can be achieved with a single-stage design.
Two-Stage Liquid Ring Pumps: These pumps use two compression stages to achieve deeper vacuum levels than comparable single-stage configurations. They are useful for processes with more demanding vacuum requirements.
Single-Stage vs Two-Stage Liquid Ring Vacuum Pumps
Liquid Ring Vacuum Pumps are available in single-stage and two-stage configurations.
Single-Stage Liquid Ring Pumps: These pumps compress gas through one pumping stage. They are suitable for many general industrial vacuum applications where the required operating vacuum can be achieved with a single-stage design.
Two-Stage Liquid Ring Pumps: These pumps use two compression stages to achieve deeper vacuum levels than comparable single-stage configurations. They are useful for processes with more demanding vacuum requirements.
Important Maintenance Tips for Liquid Ring Vacuum Pumps
Regular maintenance helps maintain pump performance and minimise unexpected downtime. Consider the following maintenance practices:
- Inspect the operating liquid: Check the liquid supply, temperature, and quality according to the manufacturer’s recommendations.
- Monitor vacuum performance: Investigate unexpected changes in suction pressure or pumping capacity.
- Check for leaks: Inspect connections, seals, and pipework for potential air or liquid leakage.
- Listen for unusual noise: Unexpected vibration or noise may indicate mechanical or operating issues.
- Inspect strainers and filters: Remove accumulated contaminants that could restrict the operating liquid supply.
- Follow servicing schedules: Inspect bearings, seals, motors, and other components according to the equipment manufacturer’s instructions.
Proper maintenance and suitable operating conditions can help extend equipment service life and maintain reliable performance.
Final Thoughts: Find Reliable Liquid Ring Vacuum Pumps in Australia
Choosing the right industrial vacuum equipment requires technical knowledge, suitable product selection, and dependable supplier support.
PumpAir Solutions offers a range of Liquid Ring Vacuum Pumps from recognised manufacturers, including Pompetravaini and Gardner Denver Nash. With over 50 years of industry experience, PumpAir Solutions supports Australian businesses with a broad selection of blower and vacuum equipment, engineering expertise, and application-focused solutions.
Whether you need vacuum equipment for chemical processing, food production, manufacturing, or wastewater treatment, the team can help you explore suitable Liquid Ring Pumps for your operational requirements.
Frequently Asked Questions
They are used for industrial vacuum applications involving gases, moisture, and condensable vapours. Common industries include chemical processing, food production, pharmaceuticals, manufacturing and wastewater treatment.
Water is commonly used as the operating liquid. However, other compatible liquids may be used depending on the process gas, temperature and equipment design.
Yes. Many models are designed for continuous industrial operation when supplied with the correct operating liquid and maintained according to manufacturer recommendations.
Single-stage pumps use one compression stage, while two-stage pumps use two stages to achieve deeper vacuum levels in suitable operating conditions.
Service frequency depends on operating conditions, liquid quality, equipment design, and manufacturer recommendations. Regular inspections help identify potential problems early.
PumpAir Solutions supplies Liquid Ring Vacuum Pumps from established manufacturers, including Pompetravaini and Gardner Denver Nash, for industrial applications across Australia.